Peptide Lyophilization Scale-Up: From Laboratory Cycle to Commercial Dryer
A practical transfer framework for vial heat transfer, dried-layer resistance, freezing differences, load mapping and comparability evidence.
A practical transfer framework for vial heat transfer, dried-layer resistance, freezing differences, load mapping and comparability evidence.
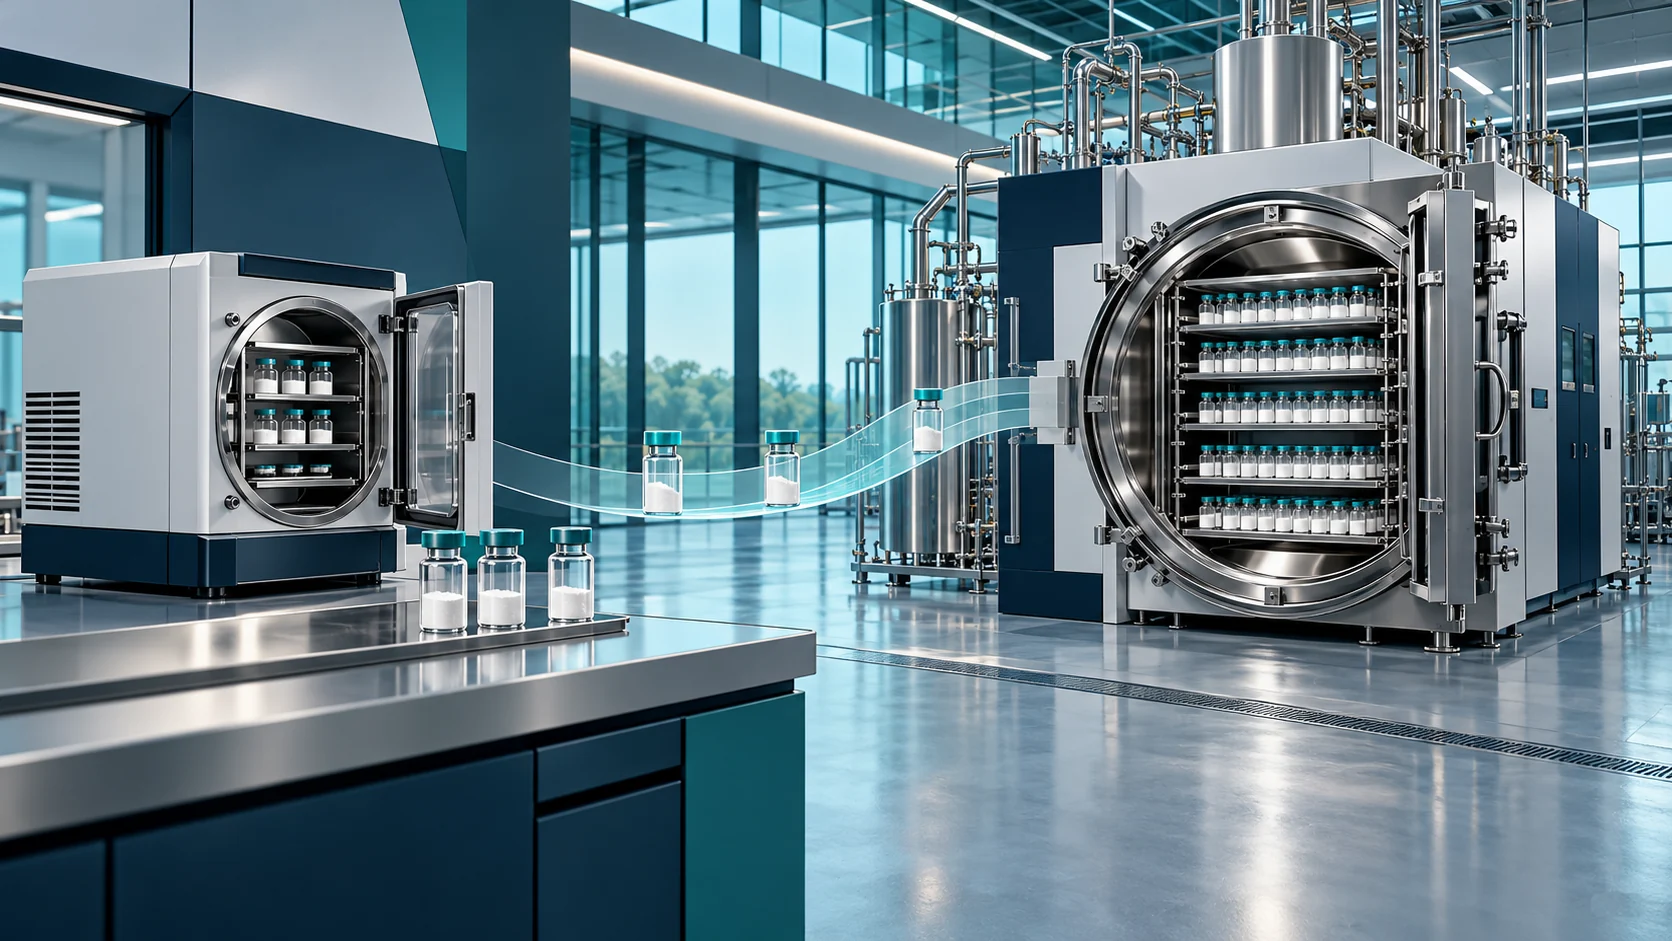
Scaling a peptide lyophilization cycle means transferring product conditions, not copying shelf-temperature and chamber-pressure settings. A laboratory cycle can behave differently in a production dryer because vial heat transfer, condenser and pressure-control capacity, loading pattern and freezing history differ. Confirm the formulation’s limits and the equipment’s capability, then run documented engineering and comparability studies before routine commercial release.
A useful scale-up brief names the peptide formulation, vial and stopper, fill, batch size and critical quality attributes. Typical attributes to justify include identity, assay, impurity profile, residual moisture, cake appearance, reconstitution and container-closure performance. Their acceptance criteria must be specific to the material and intended use. A cycle is not “equivalent” merely because it finishes in the same number of hours; it is equivalent only to the extent that the agreed product attributes remain controlled. During freezing, ice nucleation and crystal growth shape the porous path through which vapor escapes. During primary drying, the product must stay within a formulation-specific structural limit while sublimation proceeds. Secondary drying then addresses remaining bound water. The freeze-drying overview and moisture guide provide the related fundamentals.
Vial heat-transfer coefficient (Kv) describes heat delivered to a vial under specified conditions. Dried-layer resistance (Rp) describes resistance to vapor flow through the cake. Together with product temperature and equipment limits, these variables inform a primary-drying design space. Edge vials may receive heat differently from center vials; a trial that samples only an easy-to-reach shelf position can miss this heterogeneity. In a published pilot-to-production study, the authors used heat-transfer and resistance measurements to bridge their equipment scales. Their numerical coefficients belong to those dryers and formulation, not to this site’s products. The broader AAPS PharmSciTech case-study series reports quality loss when set points were transferred without accounting for scale.
| Input | Why it matters | Evidence source |
|---|---|---|
| Formulation thermal behavior | Defines a product-specific primary-drying boundary | Thermal analysis and development study |
| Kv by vial position | Captures dryer and load heat-transfer differences | Equipment-specific qualification or sublimation study |
| Rp and drying endpoint | Describes vapor resistance and completion | Formulation/process study and monitoring |
| Pressure and condenser capability | Limits achievable commercial operation | Production dryer qualification |
| Edge/center finished-vial results | Tests load uniformity | Engineering and confirmation batches |
The freezing step can change when a small laboratory load becomes a densely packed commercial shelf. Vial geometry, trays, stoppering arrangement, loading time and the cleaner production environment can affect nucleation and ice structure. A different pore structure changes resistance to drying even if the programmed shelf temperature is identical. Record load maps and process traces so a later moisture or cake defect can be traced to position. Where justified, consider controlled nucleation or annealing as development variables, but evaluate their effects on the actual peptide and excipients rather than assuming they improve every formula. The published scale-up cases include vial breakage and cake changes associated with freezing differences. Their examples demonstrate risk, not universal operating parameters.
Before declaring commercial readiness, reconcile the laboratory and production formula, primary packaging, analytical methods and critical attributes. Include the production dryer identification, cycle version, load map, monitored endpoint, deviations and representative vial results. Compare edge and center vials, and test both initial quality and stability under the proposed packaging and storage. A buyer should ask which parameters were measured, which were modeled, and which remain assumptions. Keep a change-control rule for new vials, altered fill or a different dryer. The supplier-qualification guide explains how to review that evidence without treating equipment size or a generic GMP claim as proof of product-specific capability.
It may be a starting hypothesis, not proof of transfer. Confirm equipment capability, vial heat transfer, freezing behavior, drying endpoint and finished-vial quality at production scale.
They can experience different heat-transfer conditions. Position-based sampling helps reveal a load pattern that a single pooled result would hide.
No. Initial release results and ongoing stability evidence answer different questions. The intended commercial package and storage conditions need their own stability support.
Editorial scope: technical transfer principles for B2B peptide projects. No proprietary Hytanbio cycle parameters, capacity or validation results are asserted.